Material Descrition |
Designation |
preheat |
Layers of welding |
Notices about welding |
Cast iron |
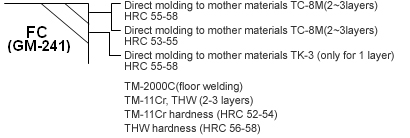
FC |
Not-required
In case of cast iron, to remove air bubbles during welding, you must preheat and remove the grease on the surface to about 800℃. |
Over 2 layers |
Single layer welding is easy to create flaws. So, avoid. |
2~3 layers |
For over 4~5mm multi-layered welding, floor welding with TC-3, TC-3A, or TC-3F is required. |
2~3 layers |
 |
FCD
(TGC-600) (GM-241)
(KSCD-800IS)
Plastic molding(KMD-800K) |
Not required
(GM-241 200℃)
In case of cast iron, to remove air bubbles during welding, you must preheat and remove the grease on the surface to about 800℃ |
Over 2 layers |
Avoid single layer welding which is easy to create flaws
TC-3F is normal in chrome treated parts.
|
2~3 layers |
For multi-layers welding over 4~5mm, floor welding such as TC-3, TC-3A orTC-3F is required. |
3 layers |
1) direct welding to mother materials with TC-8M, TC-8B, TM-11Cr, THW, and TK-3 is possible.
2) To pile TM-11Cr and THW over 3layers, floor welding with TC-3, TC-3A, TC-3F or TM-2000C is required.
TM-11Cr HRC 52~54
THW HRC 56~58 |
Heat treatment |
SKD11(HK700)
STD-11
AUD-11
KD11S |
300~350℃
(200℃) |
2~3 layers |
For over 4~5mm multi-layers welding, floor welding with TS-12G(TIG) is required. If preheating is impossible in welding parts, you must expand preheating areas to about 50mm around welded areas. Do Pooling treatment slowly after heat-treatment at about 50 Celsius higher temperature than the preheated temperature. |
350~400℃
(200℃) |
Flame treatment |
Compounded tool steel
HMD-1,5
SX105V
GO-5
Compounded case steel
ICD-1(KY870A)
(HK600-B)
ICD-5(HK600)
GO-5C
(GM-190) |
150~200℃ |
2~3 layers |
Same to Heat-treated steel |
<Remarks>
It is welding material over 40% nickel contained. You must avoid chrome plating. (the thickness of chrome is non-balanced)
TM-2000series is possible to be ionized with chrome plating..
TM-2000C-HRC 20-30
TM-2000B-HRC 37-39
TM-2000-HRC 44-46
TM-2000H-HRC 52-54 repair worn parts
TC-3-normally, welding materials for iron nickel
TC-3A-Welding materials for non-heat-treated iron nickel
TC-3F-Welding materials for iron nickel which is possible to be plated with chrome
(hardness is the same to FCD)
NIW-5 MAG Wire-HRC 55-57 |
| After annealing welded parts, flame hardening treatment should be applied to mother materials at the same time. |
150~200℃ |
2~3 layers |
Same to Heat-treated steel |
150~200℃ |
2~3 layers |
Same to Heat-treated steel |
Carbon steel
Carbon tool steel
|
S45C
SK-3 |
250~300℃ |
2~3 layers |
Same to Heat-treated steel |
Rasing severely worn blade
(the parts are often broken)
|
150~200℃ |
2~3 layers |
After welding without additional heat treatment, you can apply blade. You can acquire the best quality if you treat air-cooling at room temperature after about 2~3 hours heat treatment at 400~500℃ electric furnace. |